

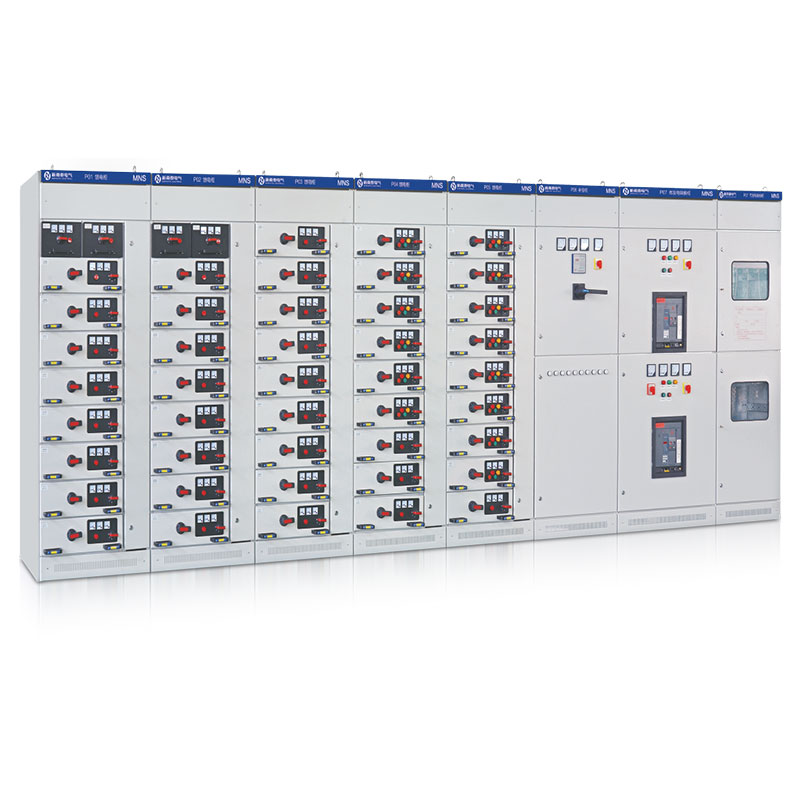


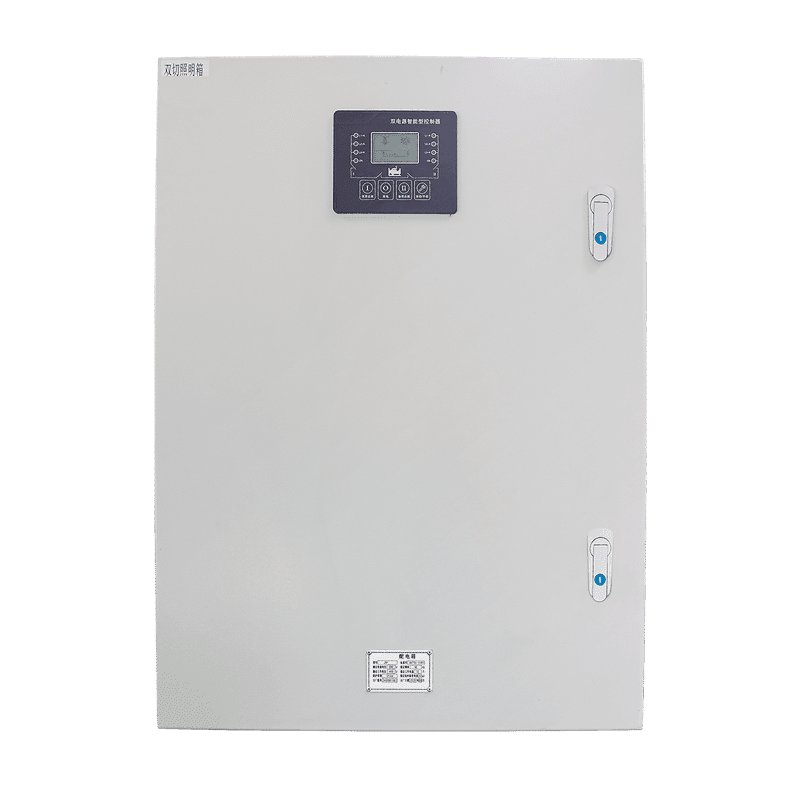


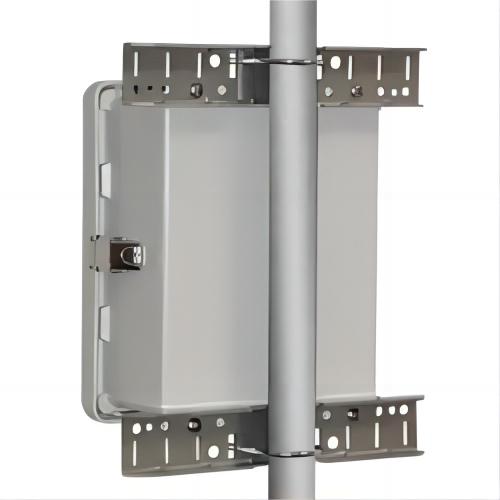


An electrical enclosure looks like the simplest item on a BOM — a steel box with a door — yet enclosure failures are among the most common root causes behind field electronics problems: condensation corrosion from wrong thermal design, gasket degradation from UV exposure, coatings that bloom white after two coastal winters, and doors that no longer seal after 200 opening cycles. Choosing among electrical enclosure manufacturers is therefore mostly about verifying rating systems, material engineering, and fabrication consistency rather than comparing box dimensions.
We manufacture enclosures and complete cabinet assemblies. This guide covers the rating landscape, the material decision matrix, and the factory-level checks that predict whether an enclosure will still be protecting your equipment in ten years.
Rating systems: the two languages you must reconcile
| System | Scope | Markers buyers actually specify |
|---|---|---|
| NEMA 250 / UL 50E (UL 50) | North American enclosure types | NEMA 1 (indoor), 12/12K (dust, dripping), 3R (outdoor, rain, sleet), 4/4X (hosedown, corrosion — 4X implies corrosion-resistant material), 7/9 (hazloc) |
| IEC 60529 (IP code) | International ingress protection | IP54, IP55, IP66 (powerful water jets), IP67 (immersion), IP69K (high-pressure/high-temperature washdown) |
| IEC 62262 (IK code) | Mechanical impact | IK08 (5 J), IK09 (10 J), IK10 (20 J) — increasingly specified for public-access and outdoor installations |
Two cautions from the manufacturing side. First, NEMA and IP do not map cleanly onto each other — NEMA types include aging, icing, and corrosion conditioning that IP tests do not, so “IP66 = NEMA 4X” claims are approximations at best (4X additionally demands corrosion resistance). Second, a rating applies to the enclosure as tested: untapped knockouts closed, doors latched, glands installed correctly. Every field modification — a drilled hole without a gasketed gland — silently voids the ingress rating.
Material selection: match the environment before comparing suppliers
- Mild steel with coating (most economical). Indoor industrial. Look for: iron-phosphate pretreatment, epoxy-polyester powder at 60–80 μm, salt-spray performance per ASTM B117 quoted as 500 h+ (indoor) or 1,000 h+ (outdoor/C4-class).
- Galvanized (Z275 or equivalent) or zinc-rich primed steel. Damp or lightly corrosive environments; also the standard substrate for painted outdoor enclosures.
- Stainless 304. Food processing, general washdown, pharma-adjacent areas.
- Stainless 316L. Coastal, chemical, offshore, high-chloride washdown — the molybdenum grade that resists pitting where 304 blooms.
- Aluminum. Light weight, good corrosion behavior, EMC-friendly; check weld quality and thickness on doors.
- Polycarbonate / fiberglass (GRP). Corrosion-free, non-conductive, lighter; favored in water treatment and outdoor telecom. Verify UV stabilization and temperature ratings for outdoor builds.
The 304-versus-316L decision is a lifecycle-cost decision: the premium for 316L is modest against the cost of replacing a corroded enclosure in a coastal plant.
Constraints settle the material question before supplier comparison begins. On a 500-unit outdoor program for a coastal industrial site — C5-M corrosion class per ISO 12944 practice, chloride plus industrial pollutant exposure — the realistic options narrow to 316L or a verified C5-class coating system on steel, and the decision should be priced per project phase, not per enclosure: with deliveries back-planned from installation milestones, a coating-system choice that demands touch-up discipline in year three is a maintenance liability the budget must own. Ask candidates for the salt-spray evidence behind whichever route they propose (1,000 h+ per ASTM B117 for this class, or mill certificates on 316L), and remember that at coastal volume the enclosure is the cheapest corrosion insurance on a site full of switchgear it protects.
Fabrication quality: what to inspect on samples
- Welding and grinding. On stainless enclosures, seams should be continuous TIG welds dressed smooth — crevices and spatter become corrosion initiation sites on an otherwise correct grade. On hygienic-area builds, surfaces are typically finished to Ra ≤ 1.2–3.2 μm (polished or linished) with no horizontal ledges.
- Gasket system. Continuous pour-in-place or formed gaskets, door closure with quarter-turn or multi-point latching that compresses the gasket uniformly. Ask the cycle life data and the compression-set behavior of the gasket material at your temperature range — this is the component that quietly dies first.
- Door and hinge hardware. Removable-pin hinges or concealed hinges with tolerances that keep the door plane true after repeated opening; latching that a gloved technician can operate. On outdoor enclosures, check for a drip-edge design over the door seam.
- Backplane and mounting. Steel subpanel fully welded or bolted with real fasteners (not sheet-metal screws), sized for your component weight; grounding boss welded to the body, not floating.
- Coating adhesion and coverage. Coverage inside cutouts and on edges — the places coaters skip are the places rust starts.
Evaluating the manufacturer beyond the product
- Rating verification evidence. Was the enclosure type-tested by the manufacturer or lab (UL 50/50E listing records, IP test reports per IEC 60529, IK per IEC 62262)? Or is the rating asserted by marking only? For hazloc (NEMA 7/9, ATEX/IECEx) the certification chain is non-negotiable and narrow.
- Fabrication capability depth. Do they make their own enclosures (laser cutting, CNC bending, welding in-house) or assemble bought-in boxes? Either can serve you, but custom sizes, special cutouts, and non-standard gland configurations are faster and cheaper at a true fabricator. Typical sheet-metal fabrication tolerance expectations: formed dimensions within ±0.2–0.5 mm class depending on size.
- Customization workflow. The professional standard: you send the component layout, they return a fabrication drawing for approval (cutout positions, gland plate, mounting plate, finish), then cut after approval. Cutting before drawing approval is where irreversible mistakes happen.
- Capacity and lead time. Standard catalog enclosures ship in days; custom fabricated runs typically 2–4 weeks; volume OEM programs with dedicated tooling compress further. Mid-size enclosure fabricators commonly produce several thousand cabinets monthly across standard and custom lines — again, the meaningful number is the committed slot for your delivery window.
- Export experience. Sea-worthy packing, desiccant, corner protection, and correct HS classification documentation (enclosures typically under heading 8538, parts for switchgear/control assemblies) prevent customs and damage friction.
FAQ
Does a higher IP rating always mean a better enclosure?
No — it means better ingress protection under the tested conditions, often with real trade-offs. Tightly sealed enclosures trap internal humidity and need condensation management (heaters, or breather/vent combinations) especially outdoors. Specify the environment, then the rating, not the reverse.
What is a gland plate and why does it matter for the rating?
The removable plate where cable glands mount. Field drilling the enclosure body instead of using the plate damages protection and grounding; a properly specified plate with correctly rated glands (IP-rated to match, EMC versions where shields must terminate 360°) preserves the system rating. Ask manufacturers to pre-machine plates to your gland schedule — a standard customization.
Stainless or coated steel for an outdoor substation enclosure in an industrial port?
316L, or coated steel in a C5-M-class system — port atmospheres combine chlorides with industrial SO2, which is aggressive on 304 and marginal coatings. The enclosure is cheap relative to the switchgear it protects.
What changes when the same decision covers 500 enclosures on a back-planned coastal schedule?
Material consistency becomes a procurement line: one mixed batch of 304 substituted into a 316L program is a decade of scattered corrosion claims. Lock mill-test-certificate delivery per heat lot into the contract, not per shipment.
Which documents protect the corrosion promise at that volume?
Mill certificates (EN 10204 3.1-type) for stainless, the coating system specification with measured dry-film thickness records for coated steel, and salt-spray test reports for the system as applied — plus staged pre-shipment photo documentation so evidence exists per delivery phase.
RFQ checklist
Environmental classification (temperature range, corrosion class, sun/UV, washdown), required rating set (NEMA/IP/IK), material and finish, internal equipment weight and heat load (for climate-control sizing), gland schedule, mounting orientation, quantity and delivery structure, and required certification documents.
Related reading
- electrical enclosure buying FAQ — the buyer-side questions this supplier guide complements.
- enclosure material selection guide — the material decision upstream of supplier choice.
- NEMA to IP converter — translate rating claims between the two systems.
Engineering note: ElectricalCabinet.net manufactures electrical enclosures and complete cabinet assemblies for industrial and export customers. This guide is an evaluation framework; enclosure selection for a specific installation should be confirmed with the responsible engineer against applicable codes.
 EN